Showing posts with label casting. Show all posts

Monday, April 26, 2010

Homemade Anvil - RR Anvil - Part 2

Part 1 talked about a home made RR-anvil which I designed, and had built with a lot of assistance from some of the guys in one of the workshops at work.

As mentioned in part 1, the issue is to stop the ringing by thickening up the web, and helping transfer any forces from the table to the base.

In an article in one of the 1920-ish shop notes from Popular Mechanics the article talked about making anvils from I-beam and thickening the web by bolting a piece of wood on each side of the web... based on that idea I made a number of pieces of 1 1/2" reinforcing steel which fitted between the rail head and the base plate of the rail.


I then cut another set of pieces which would sit between the underside of the table, and the base.


The next step was to cover the reo-bar. I used some scrap 4mm galv sheet I had kicking around. It welds easy enough, and is thick enough to stand some abuse.


The pritchel hole at the back of the anvil needed to be protected from whatever I did, so I cut up a piece of pipe to make a hollow in the back of the anvil so the underside of the hole would always be accessible.

The sheet metal shroud covered all the reinforcing bar sections welded in underneath the head, and table. Since the rail is made of high carbon Japanese steel, and my welding capabilities didn't seem to like that too much, I ensured mechanical locking whenever possible to make everything sit properly. Knowing that this would not suffice in the long run, knowing the welds made to the rail would crack under repeated hammer strikes, the next step was to fill the gaps so the reo-bar would not move under any circumstance.

The shroud was completed, with just a simple plate (about the size of a credit card) left unwelded at the back.

I obtained from the local tyre place a few bucketfuls of lead tyre weights, and melted them down using a wok burner, and one of my furnace crucibles. I could have used the furnace, but was concerned that over heating the lead might create fumes. I used the furnace when I was melting aluminium, brass and bronze since there wasn't significant issues with fumes... I was not as familiar with lead (I'm not a fishing guy who makes sinkers), so did not know how the fumes went with excessive heating. The wok burner was slower, but I figured there'd be less in the way of fumes.

Using the foundry robot, I picked up a 7L crucible of molten lead, and poured it into the gap between the shroud, and the internals of the RR-Anvil, effectively filling the gap. All surplus molten lead was poured into one of the ingot trays I use when pigging aluminium.


The lead was allowed to cool, and the final plate was recessed into the lead, and welded in place, effectively sealing in the lead. A test with the hammer and it was sweet - no ringing at all.

Here is a photo of the painted up anvil showing the recess under the pritchel hole...

And a side view of the painted anvil...

Yes, the final weight now exceeds it's original weight by more than 100%. The anvil started at 26Kg (57 lbs), and now weighs over 55 Kg (121 lbs).
The slots cut in the base web are for securing the anvil down on a wooden base, and the wonderful "imperial plum" purple paint is one of my garage sale paints I use to paint up things that need protection. I've left the top faces unpainted since it's unlikely the paint would survive the use of the horn, cutting table, and main table.

Now the anvil is finished, I've already found it too small. I've used it for a number of small jobs and for those purposes, it's fine. But once I start pointing bladeware, or other items longer than 8" at it, the table is too small. I've considered welding a larger table on top, using the existing table as a weldment anchor. I have some 2" plate here which could be used, but I'd be back at the workshops to have it cut and welded on the big machines.... I only have one small piece and I can't afford to replace it if it's spotted by a boss.

For now I limit my work in size, and am on the hunt for a decent size anvil. I'm playing with a "false table" idea to allow larger work, but that's had to take the back seat for other projects lately. The "false table" is effectively an extension of the "third hand" concept used by some smiths... a set of light gauge supports are used to retain, or hold the work on the anvil, but they aren't actually part of the anvil. All striking would still occur on the anvil, but the false table would permit me to ensure the work was level, and flat when it is on the table... still in Mk2 testing....

Saturday, April 10, 2010

Bender's eyes - the good ones

I discussed how attempting to cast the eyes from cement did not work as well as planned. Ideally I wanted weld-ments, but did not have enough of the pressure cylinders to make that work. I returned to the casting option, but with a different media than cement. If I'd been able to use my furnace, I'd have made them from aluminium to begin with, but that was not an option, so instead I chose to cast the eyes from "bog" - a.k.a. Automotive putty.

I kept the fixtures I made for the cement eyes, and the eye plates.
The idea of sand molds didn't appeal with using bog, so I looked for an alternative mold. Whilst shopping with my darling wife, I found some cheap Christmas decorations. They were plastic balls which measured 85mm across, and had a clearly defined mold line from their manufacture. I bought three of them and cut them carefully along the mold line to get hemispheres. I mixed up some bog, filled one of the hemispheres, and placed it on the eye-plate with a fixture already secured.
A couple of notes on the above procedure:

-- I've been keeping my bog in a refrigerator so it's cold, and not going off as fast. (I also keep all my glues, and expensive solvents in the same fridge)

-- I sprayed the eye-plate with a light oil as a form of mold release to stop the bog sticking to the plate... However I did not spray any oil on the fixture since I wanted maximum adhesion to this part.

-- A reasonably thick section of curing bog gets VERY hot. I'd seen similar exothermic reactions when working epoxy with the rockets, so I knew I could cool the mold from the outside with water, and not cause any damage to the casting. If anyone else tries thick castings based on resins, they should not leave the casting unattended during curing, and keep flammables away. If possible, do the casting in layers to distribute the heat effects.

Once the putty had cured, I removed the decoration halves (some popped off neatly, others needed to be cut away), and sanded out any irregularities caused by the thin plastic warping with the hot putty, or due to the weight of putty.

The end result after repeating the above with another three eye castings was two sets of eyes. I decide not to bother with making up the third eye-plate since I was running out of bog at the time.
Top view of bog eyes mounted on plate.

front view of good eyes on plate.
This photo demonstrates how the eye-plate bolts to the head. In this shot I was testing the exposed length of the eye fixtures to ensure they would not foul against the surface of the head. The eye-plates are held to the head by a single bolt on the centreline of the plate, and the head. A second "prong" is also there to prevent rotation of the eye-plate which engages with a hole located 25mm (1") below the holding bolt.

Bender's failed eyes

I won't go into too much detail on this aspect of Bender's construction, but it was something worth trying, and it may be of use to someone.
I had this one gas cylinder, it was from inside a pressurised water extinguisher. The bottom of it was a perfect hemispherical shape, and the diameter was perfect for Bender's eyes... the problem was I only had one of them.


I decided to use this one cylinder as a positive pattern, and make molds so I could replicate the hemispherical end. I cut up a scrap piece of 4" pipe for flasks, and using common packing tape to close off the bottom, half filled the pipe segments with sieved clay mixed sand. I tamped the sand down as I put it in the flask, and tamped the sand around the pattern as I sprinkled more sand in. Effectively I was creating an "open face mold" for each eye. I created six molds as shown in the photo below. The long 1/2" bolt was used for tamping the sand.

Now I had the hemispherical shape of Bender's eyes sorted, I needed a way to attach them to the rest of his head. I'd designed the use of an "eye-plate" which would bolt to the rest of his head, and essentially be a carrier for the eyes. This design made fabrication easier, and allowed for other features such as "clip on eyelids". To attach the eyes to the eye-plate, I made up some fixtures which were basically a 1/4" bolt, with some heavy wire welded to it. One leg of the wire was bent parallel to the bolt, and presented 15mm (~5/8") away from the bolt centre. This leg was to stop the eye rotating around the bolthole when fixed to the eye-plate. The rest of the wire was simply bent in a loose loop to be encased in the eye casting. The photo below shows a row of bolts, having their heads welded to the wire loops, holes drilled in the aluminium extrusion maintains the spacing of the bolt and the wire prong.

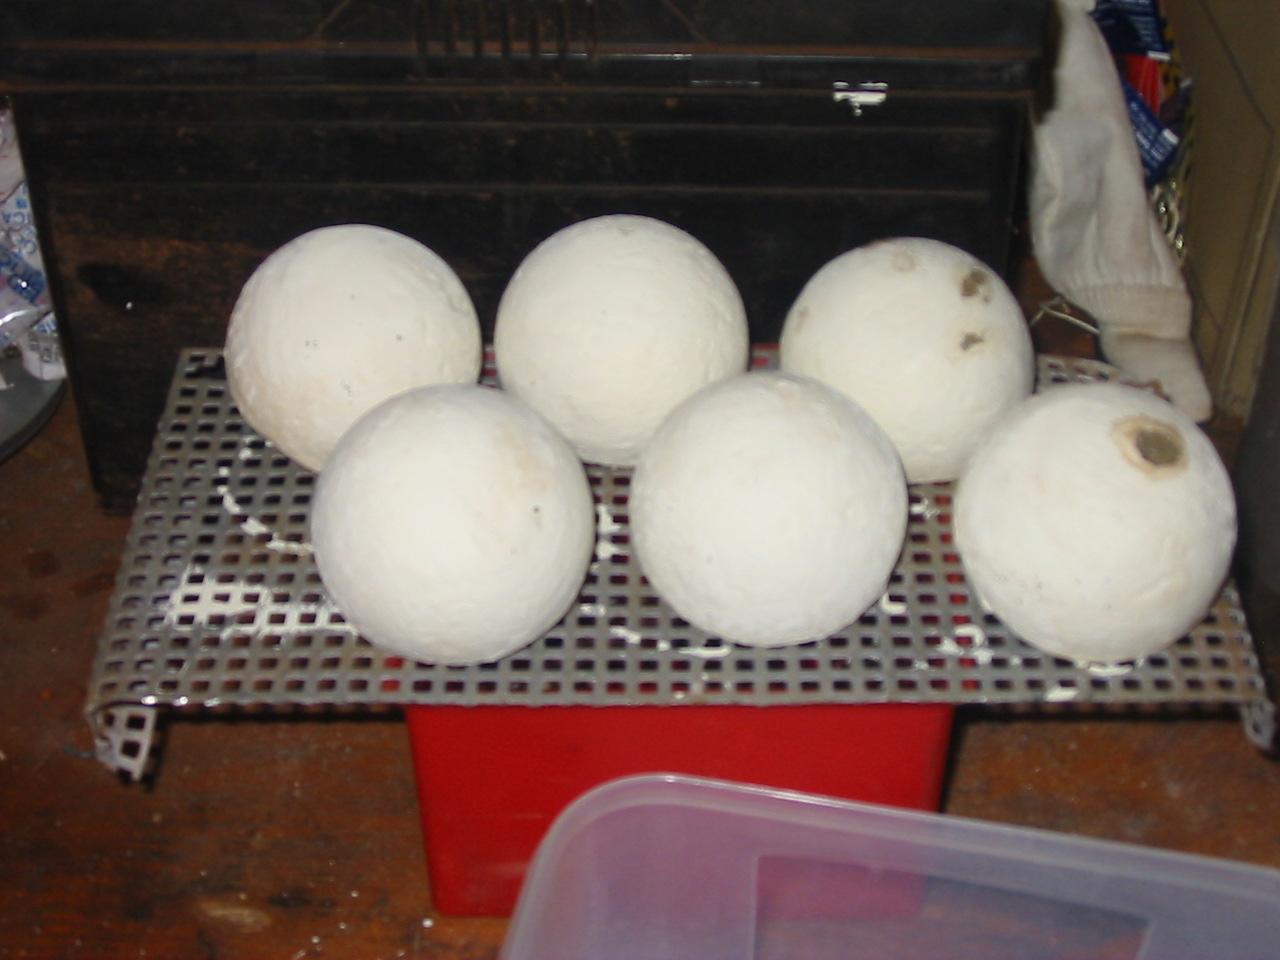
The molds were then filled with "post mix" cement, and the bolt/wires fixtures were inserted. The cement was left over from another job, and used pretty much straight from the bag, but I'd sieved out the larger aggregate so it'd flow better in the molds, and not have any inclusions.

Once the cement had cured, I removed them from the sand molds, and cleaned them up, and sealed them with sealer undercoat paint. I had a hiccup when two of the eye rolled whilst the paint was drying, and stuck to the benchtop, when I pulled them off, the paint pulled out of the cement - this was a warning of what was to come.

Maybe the cement was old, maybe removal of the aggregate did something, maybe the phase of the moon was wrong, maybe the mix was too wet, maybe, maybe, maybe - whatever the reason, the eyes were too fragile. I found I could "cut" them with my thumb nail, and I accidently dropped one of the eye-plates when it was loaded with the eyes, and the eyes flew apart. (see photo below)
Based on that, I decided cement eyes were not going to work. I retained the eye fixtures, plates, and started looking for a better method. What worked was only a minor deviation from this plan, but it worked well.