Showing posts with label scrap. Show all posts

Monday, April 26, 2010

Homemade Anvil - RR Anvil - Part 2

Part 1 talked about a home made RR-anvil which I designed, and had built with a lot of assistance from some of the guys in one of the workshops at work.

As mentioned in part 1, the issue is to stop the ringing by thickening up the web, and helping transfer any forces from the table to the base.

In an article in one of the 1920-ish shop notes from Popular Mechanics the article talked about making anvils from I-beam and thickening the web by bolting a piece of wood on each side of the web... based on that idea I made a number of pieces of 1 1/2" reinforcing steel which fitted between the rail head and the base plate of the rail.


I then cut another set of pieces which would sit between the underside of the table, and the base.


The next step was to cover the reo-bar. I used some scrap 4mm galv sheet I had kicking around. It welds easy enough, and is thick enough to stand some abuse.


The pritchel hole at the back of the anvil needed to be protected from whatever I did, so I cut up a piece of pipe to make a hollow in the back of the anvil so the underside of the hole would always be accessible.

The sheet metal shroud covered all the reinforcing bar sections welded in underneath the head, and table. Since the rail is made of high carbon Japanese steel, and my welding capabilities didn't seem to like that too much, I ensured mechanical locking whenever possible to make everything sit properly. Knowing that this would not suffice in the long run, knowing the welds made to the rail would crack under repeated hammer strikes, the next step was to fill the gaps so the reo-bar would not move under any circumstance.

The shroud was completed, with just a simple plate (about the size of a credit card) left unwelded at the back.

I obtained from the local tyre place a few bucketfuls of lead tyre weights, and melted them down using a wok burner, and one of my furnace crucibles. I could have used the furnace, but was concerned that over heating the lead might create fumes. I used the furnace when I was melting aluminium, brass and bronze since there wasn't significant issues with fumes... I was not as familiar with lead (I'm not a fishing guy who makes sinkers), so did not know how the fumes went with excessive heating. The wok burner was slower, but I figured there'd be less in the way of fumes.

Using the foundry robot, I picked up a 7L crucible of molten lead, and poured it into the gap between the shroud, and the internals of the RR-Anvil, effectively filling the gap. All surplus molten lead was poured into one of the ingot trays I use when pigging aluminium.


The lead was allowed to cool, and the final plate was recessed into the lead, and welded in place, effectively sealing in the lead. A test with the hammer and it was sweet - no ringing at all.

Here is a photo of the painted up anvil showing the recess under the pritchel hole...

And a side view of the painted anvil...

Yes, the final weight now exceeds it's original weight by more than 100%. The anvil started at 26Kg (57 lbs), and now weighs over 55 Kg (121 lbs).
The slots cut in the base web are for securing the anvil down on a wooden base, and the wonderful "imperial plum" purple paint is one of my garage sale paints I use to paint up things that need protection. I've left the top faces unpainted since it's unlikely the paint would survive the use of the horn, cutting table, and main table.

Now the anvil is finished, I've already found it too small. I've used it for a number of small jobs and for those purposes, it's fine. But once I start pointing bladeware, or other items longer than 8" at it, the table is too small. I've considered welding a larger table on top, using the existing table as a weldment anchor. I have some 2" plate here which could be used, but I'd be back at the workshops to have it cut and welded on the big machines.... I only have one small piece and I can't afford to replace it if it's spotted by a boss.

For now I limit my work in size, and am on the hunt for a decent size anvil. I'm playing with a "false table" idea to allow larger work, but that's had to take the back seat for other projects lately. The "false table" is effectively an extension of the "third hand" concept used by some smiths... a set of light gauge supports are used to retain, or hold the work on the anvil, but they aren't actually part of the anvil. All striking would still occur on the anvil, but the false table would permit me to ensure the work was level, and flat when it is on the table... still in Mk2 testing....

Friday, April 9, 2010

Grabby & Squeezy - Hands part 1

Grabby and Squeezy - these are the names of Bender's hands.

Knowing how important Bender's hands are to him, I spent a lot of time trying to figure out the best way to build them.

I'd been collecting his fingers for ages - the fingers are discharged CO2 cylinders from life jackets. I tripped over some at work one day and recognised the shape. The guys on shift, and maintenance saved them for me and I ended up with enough to make 4 hands. I'm retaining the spare fingers in the hope of redesigning the hands in the future.

As with everything else in Bender, I started with scrap 4mm galv sheet. I marked out a number of disks, 2 to match the diameter of the arm pipe, 2 to match the inside diameter of the hand, and 2 to match the diameter of the flared hand. The largest plate (flared diameter) was then marked out with 3 radially spaced holes to match the diameter of the Co2 cylinders. (finger plate)
A central hole was also drilled in all plates for the retaining bolt.


The above photo shows the components which make up the hand. From left to right across the edge of the welding table the parts are; Arm plate with captive nut, wrist plate, captive retaining bolt, pipe spacer, finger plate, 3 fingers.
The retaining bolt has had the threads nearest the head undercut so the bolt can spin in the wrist plate and not fall out, or bind. The spacer pipe seperates the wrist and finger plates.
The pieces above the components on the table include the made up shroud, but that will be discussed more in the next page (part 2).


The components assembled. The arm plate has been welded to the end of the arm, the wrist and finger plates welded to the spacer pipe with the retaining bolt already captive in the wrist plate prior to welding. The fingers were set through the holes, with a moderate degree of flaring, and then welded in place. Another view of the the assembled hand structure is shown below...

Part 2 of "Grabby and Squeezy" will cover the construction and fitting of the shroud, and placing the hands on the arms.

Bender's foundations - feet, legs, base - part 1

The foundation, the base, what holds Bender up.

I started with the largest piece of scrap sheet I had which was 4mm thick. It's about 900x600mm (3' x2') and marked it up so Bender would be standing with his feet centered 150mm (6") back from the centre-line. I made him off-centre since I determined his center of gravity would always be forward of his center-line due to the positioning of his arms, the door being opened, and the weight offset in the head (weight of eyes, shroud).

I also decided his feet cups would not actually rest on the plate directly. I decided this based on trying to prevent rust from moisture being trapped there, and to give me the option of covering the base plate with sand, cement, or some other covering to disguise it. The gap under the foot cups is about 6mm (1/4"). So how are the feet attached to the base?

The foot cups are simply the tops of 9kg(20lb) NuSwift DCP extinguishers, appropriately cut, patched and positioned to make the feet. The NuSwifts used to have a large bronze valve at the very top containing the release disk, hose port, and carry handle. The valve casting screwed into the top of the extinguisher via a large bronze pressure fitting which was brazed inside the body of the extinguisher. In the above photo a gutted valve has been turned upside down and bolted to the base plate. A small piece of steel has been welded to the baseplate between the handle lugs to prevent the valve from turning on the retaining bolt. The foot cups are then simply screwed onto the valve from the underside with only the bolt and spacer protruding above the cup. By locking the rotation of the valve, and marking the feet ( The chalk "R" inside the cup) the feet can be repeatedly placed on the baseplate the exact same way.

The above two photos show my first attempts at making the legs from short sections of extinguishers cut and welded at angle to approximate the curved legs. - I know I could have made them straight like Simon did at asciimation, but I wanted to make mine curved since it seemed more natural and "in character". After many frustrating attempts at trying to make the legs from the extinguisher sections, I thought of a better way, and cut the old attempts away from the feet and pitched them in the trailer for the tip.


The new legs... "Captain Dan, you've got new legs" - sorry couldn't resist....
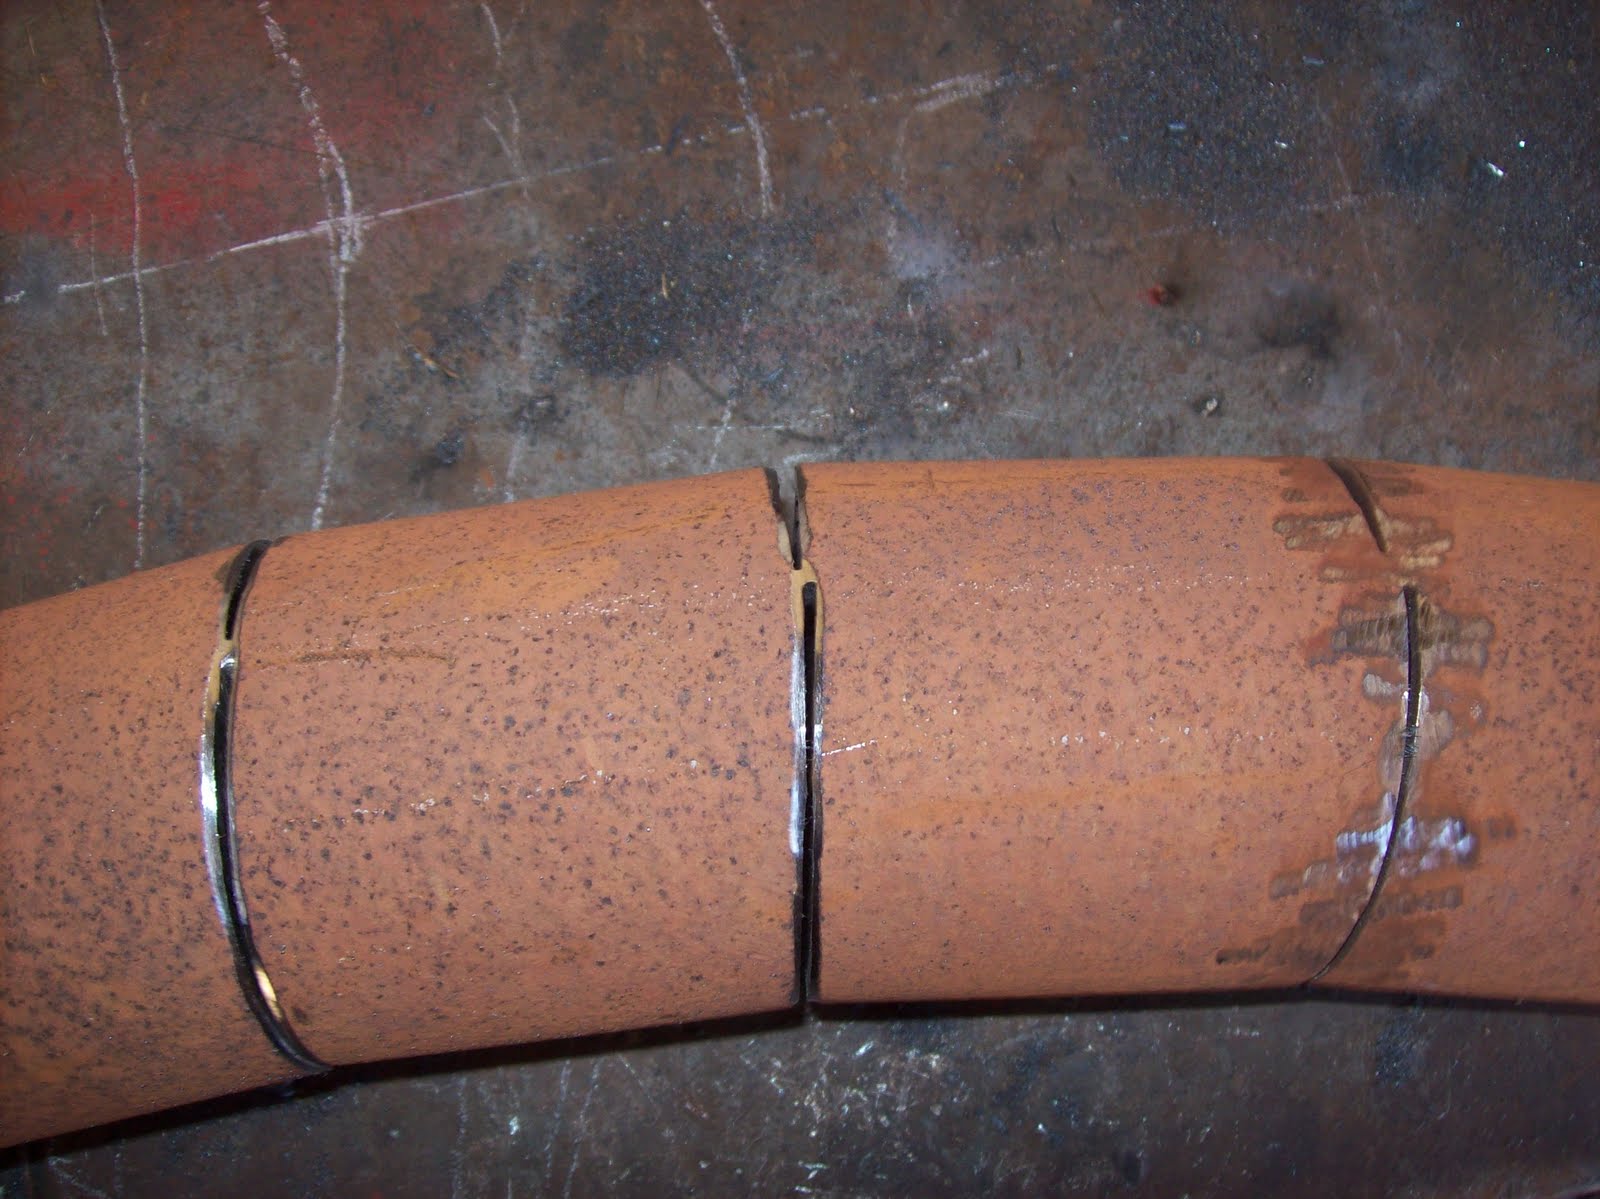
The new legs were made from some pipe I scored from some friends at work. Apparently it was leftover from some obscure job and didn't suit anything around the plant. It was an odd size - 83mm OD (about 3 1/2") and only 2 mm larger than my plans called for. I marked the centre-line of the pipe, and called that 12 o'clock. I then marked lines at 2 and 10 o'clock. this divided the circumference of the pipe into two sections, one of 60 degrees, the other of the remaining 300 degrees. I then marked out the regular segments based on the spacing being equal to the diameter. I had originally thought to have the welds visible for the legs and arms, but later ground them flush.
With the marks all in place, I used a 2.2mm cutting disk to cut the 300 degree segment lines. I then left about 1mm (1/16") of connected steel, and used a 1mm disk to cut the 60 degree segment lines. This allowed me to "bend" the pipe so the 2.2mm cuts closed on themselves, and the gaps at the 1mm cuts only marginally increased. The resulting curve is shown below, with some minor grinding to prepare for welding.


A note about my welding... I've been asked what kind of welder I have. It's a common cheap arc welder - 240VAC "buzz box" using 2.5mm SatinCraft welding rods. I'd love to have a MIG welder, but that will have to wait for another day. I did try learning how to use a MIG welder several years ago, but I'd got so used to controlling my arc by my own hand, I kept moving the handpiece and not compensating for the wirefeed. Learning to MIG is on the "to do" list, but a long way down whilst the stick welder does what I need.